 |






| Quantity: | |
|---|---|
EP100 EP125 EP200 EP250 EP300 EP350 EP400 EP500 EP600
100 meters
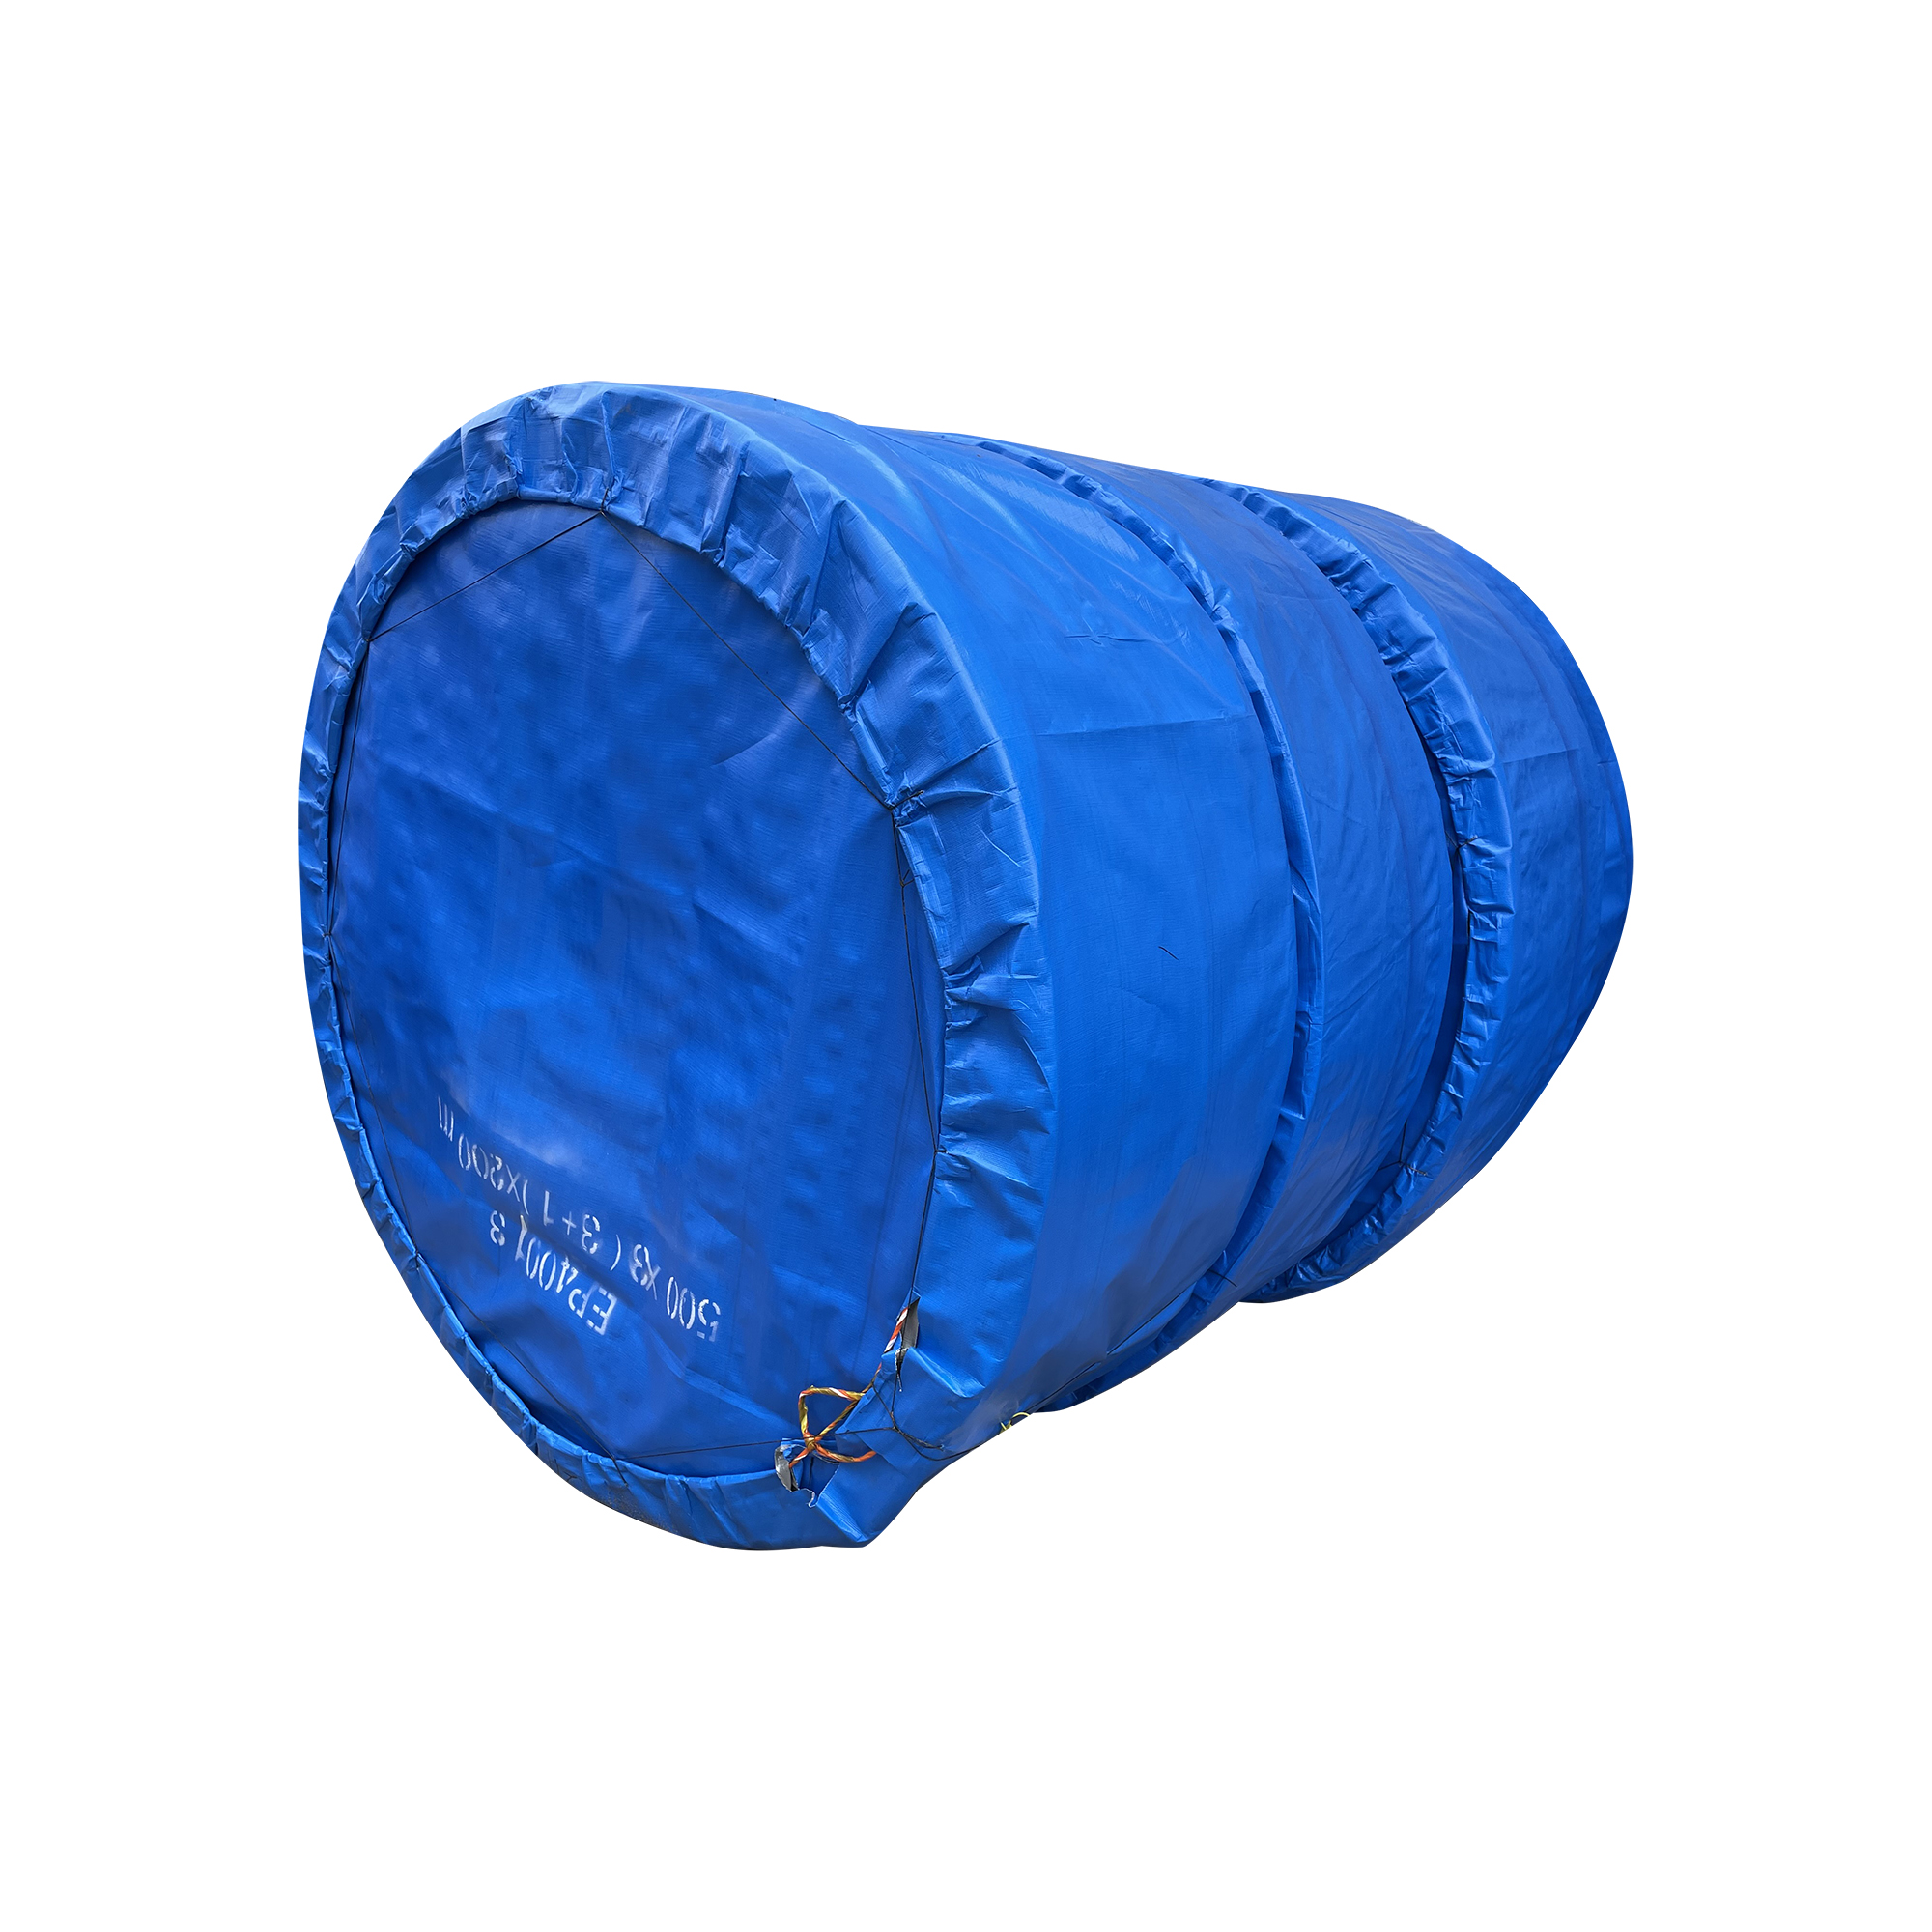
EP conveyor belts derive their designation from the polyester-polyamide (EP) fabric carcass that forms the belt's tensile layer. This construction combines polyester warp yarns with polyamide weft yarns, creating a fabric reinforcement that delivers specific mechanical properties suited for bulk material handling applications. The chemical resistant variant incorporates cover compounds formulated to withstand exposure to various chemical substances.
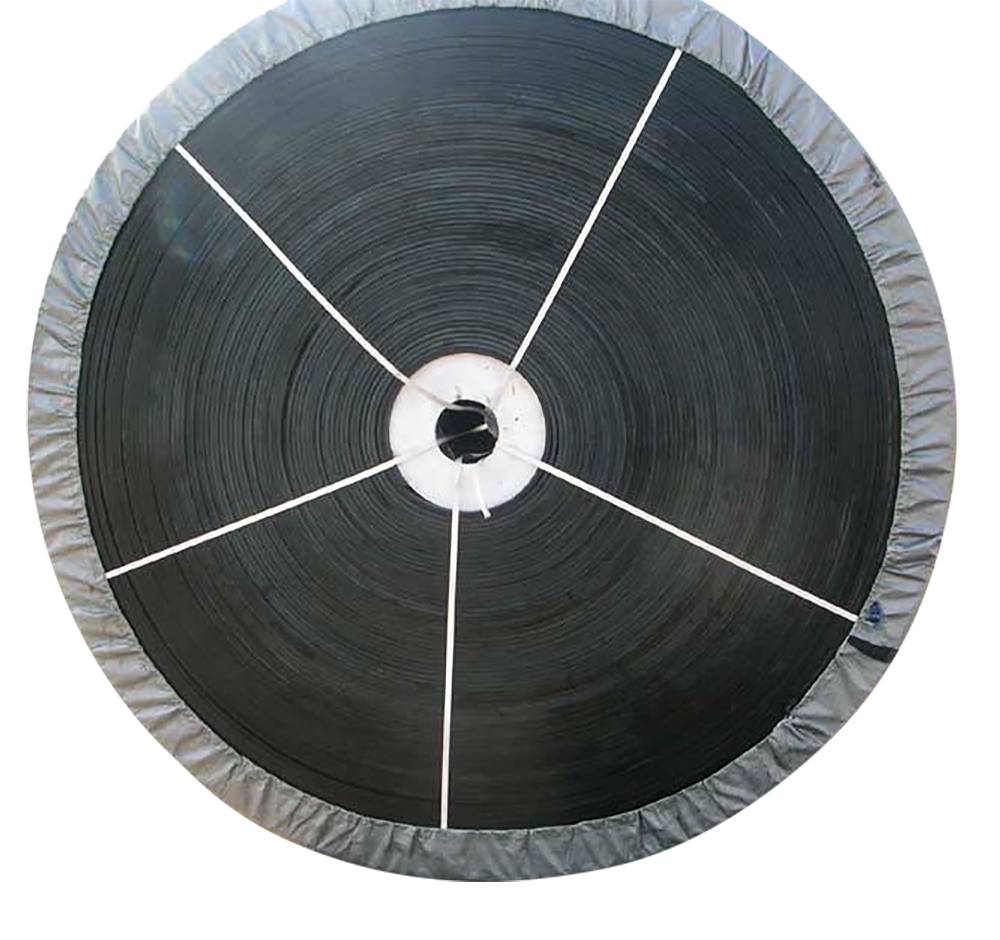
The EP carcass consists of multiple plies of woven fabric where the warp threads (running along the belt length) are polyester and the weft threads (running across the belt width) are polyamide. This combination produces a belt with high tensile strength in the lengthwise direction while maintaining good transverse flexibility. The fabric plies are bonded together with skim rubber compounds that ensure uniform load distribution across the belt width.
The chemical resistant feature of these conveyor belts comes from specialized rubber cover compounds applied to the carrying and pulley covers. These formulations resist degradation when exposed to chemical substances, including acids, alkalis, and various industrial chemicals encountered in material handling processes. The covers also provide erosion resistance against water and steam, supporting performance in wet or humid operating environments.

EP conveyor belts offer a combination of mechanical properties that make them suitable for a wide range of material handling scenarios, particularly where chemical exposure and long-distance transport are involved.
EP conveyor belts have high tensile strength relative to their weight, allowing thinner and lighter belt constructions compared to some alternative carcass types. The polyester warp fibers contribute to low elongation under load, meaning the belt maintains its length more consistently during operation and requires less frequent tensioning adjustments. This low elongation characteristic supports stable conveyor operation over long distances.
The belt construction provides good impact resistance, helping it absorb the force of materials being loaded onto the conveyor surface. The polyamide weft contributes to excellent groove formation ability, allowing the belt to conform properly to troughing idler configurations. Good troughability ensures that the belt maintains its shape across the idler set, reducing the risk of material spillage and supporting stable tracking.
EP belts demonstrate good stability when heated, meaning their physical properties remain relatively consistent across a range of operating temperatures. The combination of fatigue resistance, wear resistance, and chemical resistance contributes to long service life in appropriate applications. These characteristics make EP chemical resistant belts a developing trend in fabric conveyor belt technology for industrial applications.
EP chemical resistant conveyor belts are primarily used in harsh conditions involving long-distance material transport where chemical exposure is present. Their combination of properties supports reliable performance in various industrial settings.
In chemical processing plants, these belts handle materials that may contain acidic, alkaline, or other chemically active components. Applications include transporting chemical powders, granular fertilizers, salt, and other corrosive bulk materials. The chemical resistant covers help maintain belt integrity when exposed to substances that would degrade standard rubber conveyor belt covers.
Mining operations use EP conveyor belts for long-haul transport of ores and minerals where chemical leachates or process chemicals may come into contact with the belt surface. The belts handle the mechanical demands of heavy mineral loads while resisting chemical attack from process waters and reagents. Their low elongation property is particularly beneficial for long conveyor lines where stretch management is critical.
Agricultural fertilizer production and handling facilities specify EP chemical resistant belts for moving ammonium nitrate, urea, potash, and other fertilizer products that can be corrosive to standard rubber compounds. The belts support both transport and processing operations within fertilizer plants, from raw material intake to finished product loading.
EP chemical resistant conveyor belts are available in multiple strength grades to match different load requirements and conveyor lengths.
The available models include EP100, EP125, EP200, EP250, EP300, EP350, EP400, EP500, and EP600. The numerical designation corresponds to the belt's full-thickness tensile strength in newtons per millimeter of belt width. Higher numbers indicate greater tensile strength, suitable for longer conveyors, heavier loads, or steeper inclines. Selecting the appropriate grade involves calculating the required tensile strength based on conveyor length, lift, material weight, and safety factors.
The minimum order quantity for EP chemical resistant conveyor belts is 100 meters. This threshold allows for custom cutting and splicing to specific conveyor lengths while maintaining manufacturing efficiency. For commercial procurement, buyers should measure their conveyor system accurately and account for splice lengths when determining the required belt length.
Selecting the correct EP chemical resistant conveyor belt involves evaluating several technical factors to ensure proper fit and performance in specific operating conditions.
Key factors in belt selection include required tensile strength (determining the EP grade), cover thickness (based on material abrasiveness), chemical exposure type and concentration, operating temperature range, belt width, and conveyor length. Consulting with engineering teams or supplier technical representatives can help match belt specifications to application requirements.
For enterprise customers making commercial procurement decisions, suppliers that provide material specification sheets, test reports, and certification documentation support more confident purchasing. Documentation may include tensile strength test results, cover thickness measurements, chemical resistance test data, and splice procedure guidelines. Verified quality standards reduce the risk of premature belt failure and support more predictable maintenance planning for business operations.
EP stands for polyester-polyamide, referring to the fabric carcass construction where the warp threads are polyester and the weft threads are polyamide. This combination delivers specific mechanical properties including high tensile strength and low elongation.
Chemical resistance varies by specific cover compound formulation. Generally, these belts resist exposure to acids, alkalis, and various industrial chemicals. The exact resistance profile should be verified with the supplier based on the specific chemicals in your application.
The EP grade selection depends on the required tensile strength, which is calculated based on conveyor length, lift height, material weight per meter, belt speed, and safety factors. Higher EP numbers indicate greater tensile strength for heavier loads or longer conveyors.
The minimum order quantity is 100 meters. Custom lengths can be provided based on specific conveyor measurements and splice requirements for industrial applications.