 |






| Quantity: | |
|---|---|
EP100 EP125 EP200 EP250 EP300 EP350 EP400 EP500 EP600
100 meters
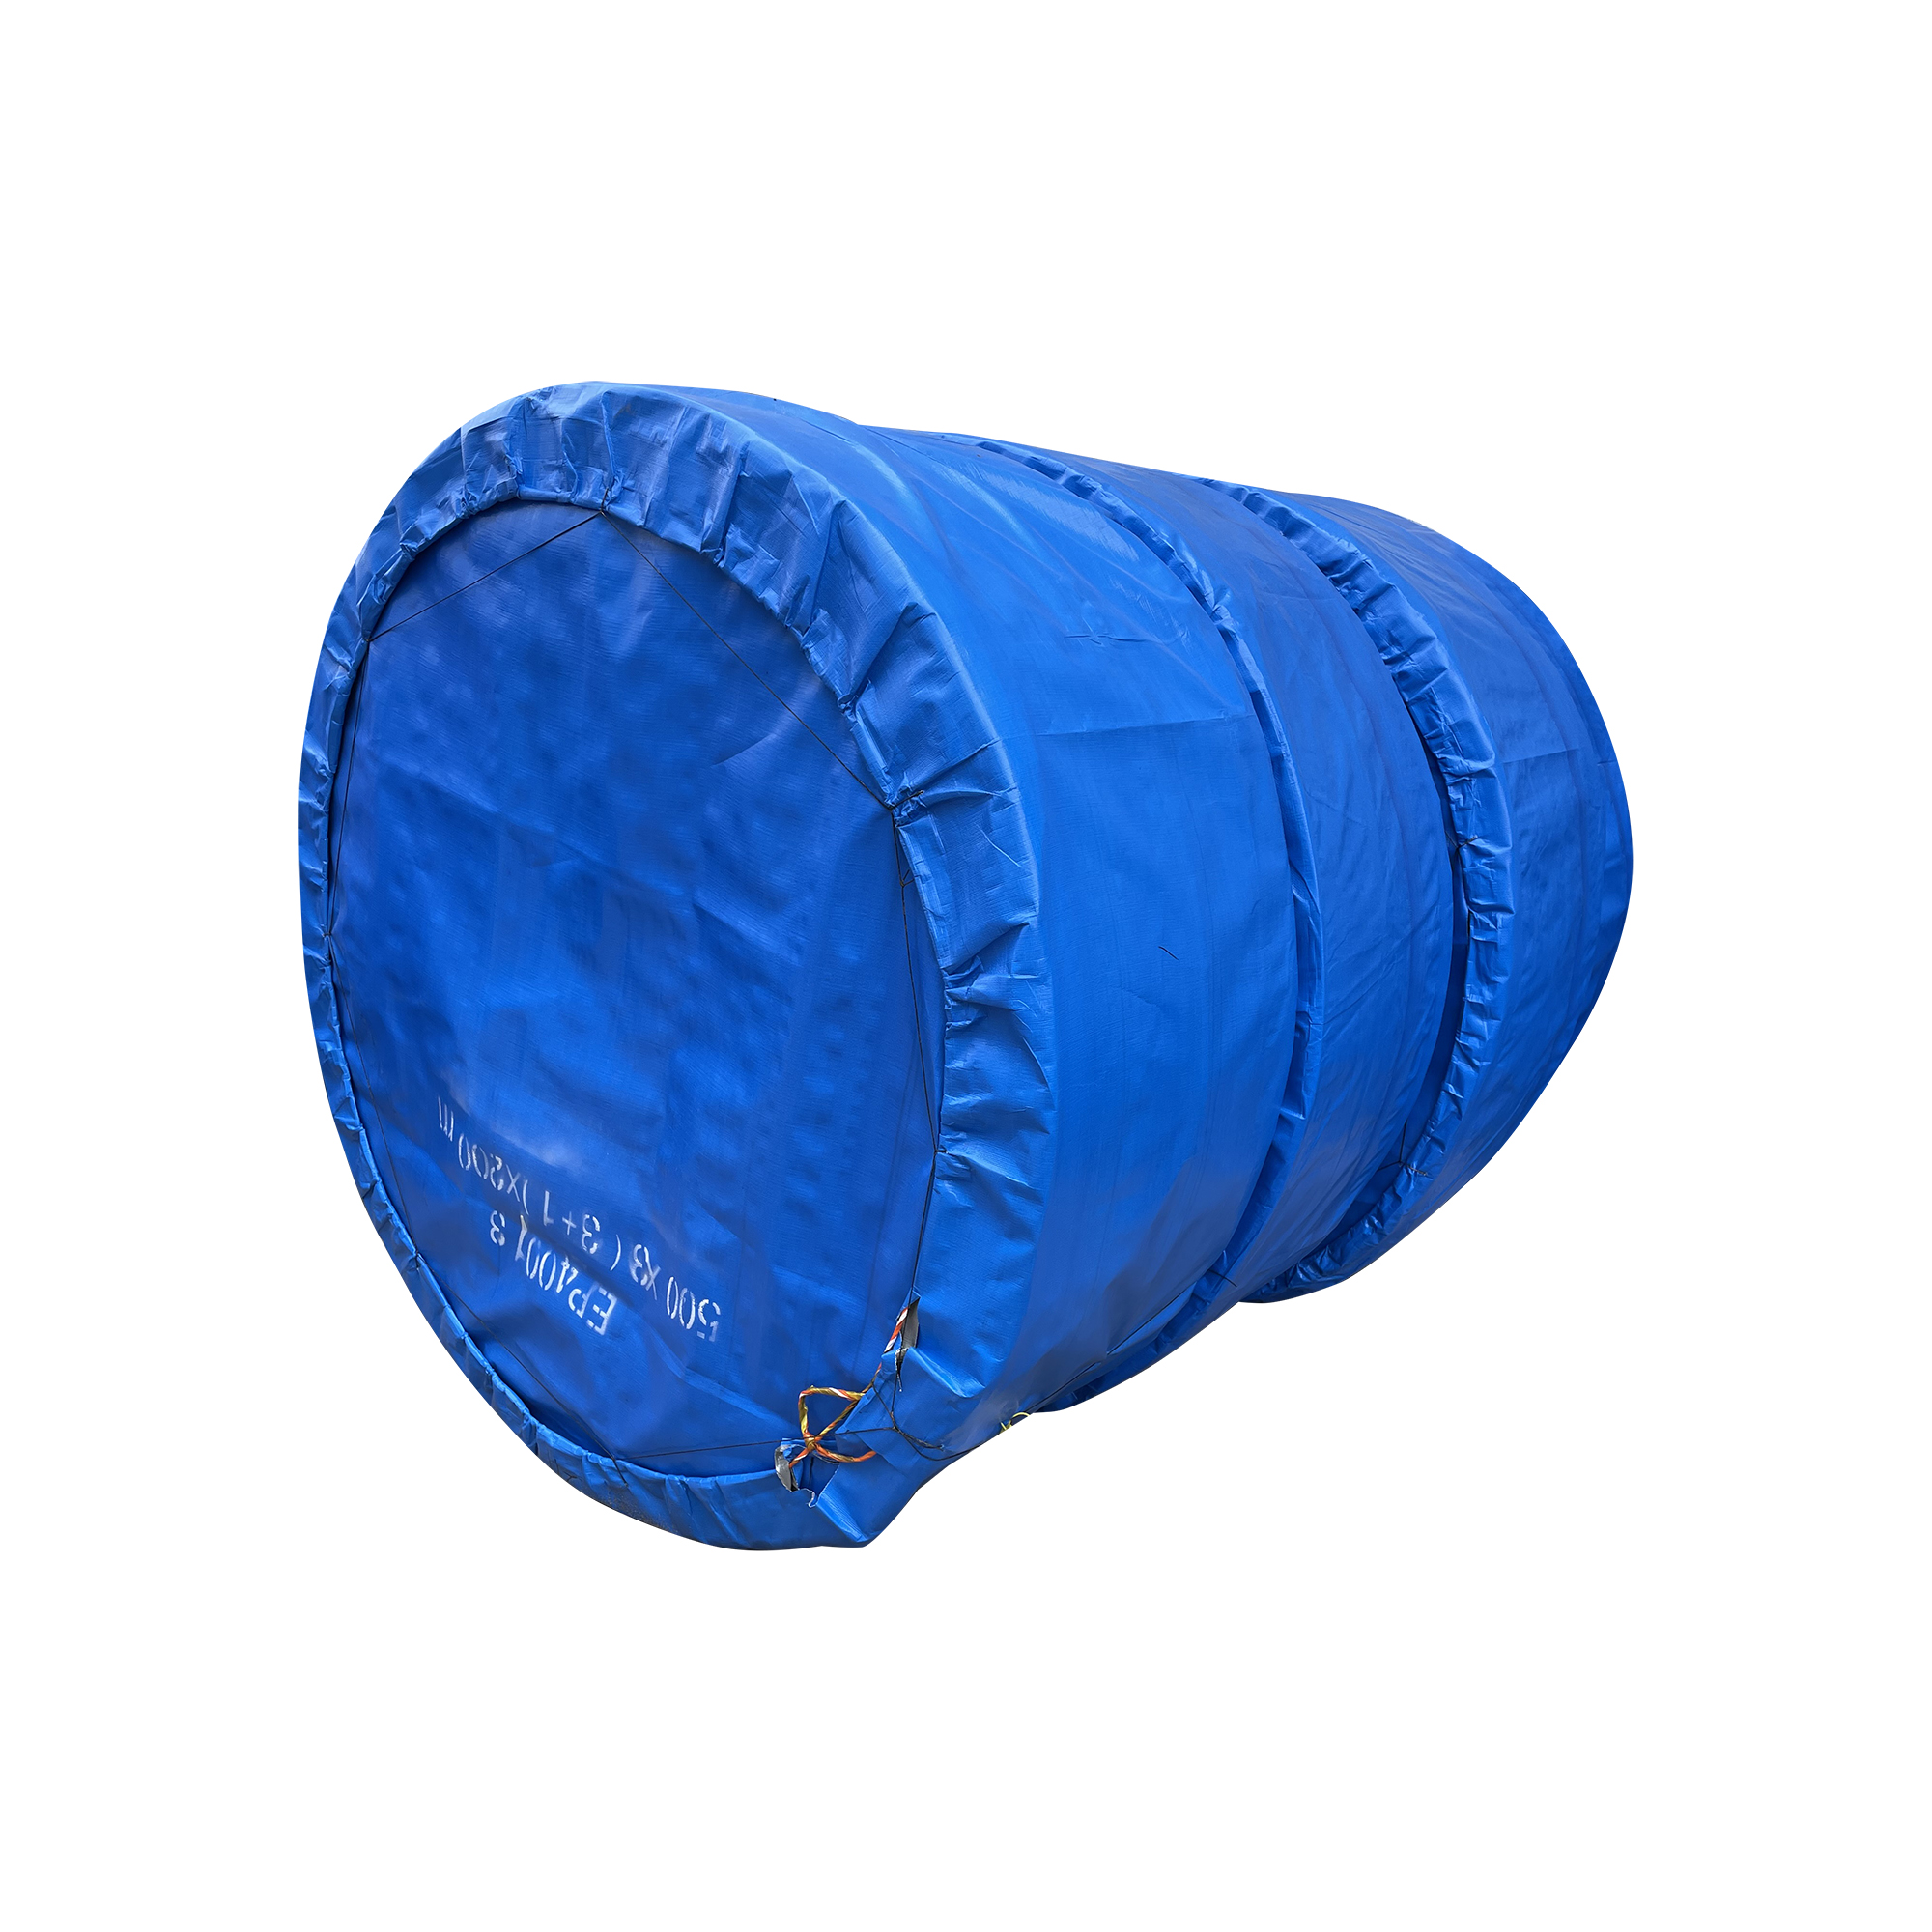
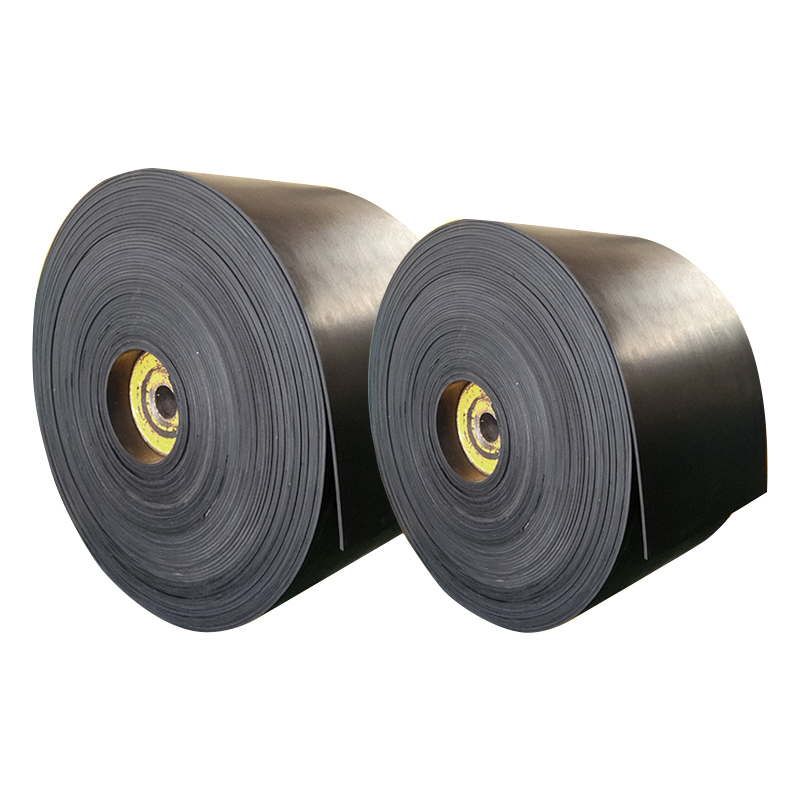
Cold resistant conveyor belts use polyester warp and nylon weft (EP) fabric as the tensile reinforcement layer. The EP fabric provides high tensile strength, low elongation, and dimensional stability under load conditions. Multiple plies are bonded together with a rubber skim compound to form the carcass, with the number of plies determined by the required tensile strength rating from EP100 through EP600.
The top and bottom rubber covers are formulated with cold-resistant compounds based on neoprene, EPDM, or specialized synthetic rubber blends. These compounds maintain flexibility and impact resistance at sub-zero temperatures where standard rubber compounds become brittle. The cover thickness is specified according to the material being conveyed and the severity of the service conditions.
Belt edges are sealed with a rubber compound to prevent moisture ingress and delamination at the cut edges. For cold environment applications, edge sealing provides additional protection against freeze-thaw cycles that could affect the fabric carcass. Edge treatment options include cut edges, molded edges, or reinforced edge constructions depending on application requirements.

Grade | Full Thickness Tensile Strength (N/mm) | Elongation at Break (%) | Cover Thickness (mm) | Operating Temperature |
|---|---|---|---|---|
EP100 | 100 | ≥ 10 | 1.5 × 4.5 | -40°C - 50°C |
EP125 | 125 | ≥ 10 | 1.5 × 4.5 | -40°C - 50°C |
EP200 | 200 | ≥ 10 | 2.0 × 5.0 | -40°C - 50°C |
EP250 | 250 | ≥ 10 | 2.0 × 5.0 | -40°C - 50°C |
EP300 | 300 | ≥ 10 | 3.0 × 6.0 | -40°C - 50°C |
EP400 | 400 | ≥ 10 | 3.0 × 6.0 | -40°C - 50°C |
EP500 | 500 | ≥ 10 | 4.0 × 8.0 | -40°C - 50°C |
EP600 | 600 | ≥ 10 | 4.0 × 8.0 | -40°C - 50°C |
In cold climate mining operations, cold resistant conveyor belts transport ore, coal, and aggregate materials through outdoor environments with sub-zero temperatures. The belts maintain flexibility and impact resistance during winter months, supporting continuous material handling in regions with seasonal freezing conditions.
Food processing facilities and cold storage warehouses use cold resistant conveyor belts for product movement through freezer and chilled storage areas. The belts remain flexible at low temperatures, ensuring consistent operation around pulleys and rollers within cold storage environments.
Port terminals and logistics yards in cold climate zones deploy cold resistant conveyor belts for bulk material handling. These belts withstand exposure to wind, moisture, and freezing temperatures while maintaining structural integrity during continuous operation.
Grain elevators, fertilizer handling facilities, and agricultural processing plants in cold regions use cold resistant belts for seasonal and year-round material transport. The belts resist cracking and stiffening in low-temperature conditions, supporting harvest and processing schedules through winter months.
The primary characteristic of cold resistant conveyor belts is their ability to maintain flexibility at temperatures below freezing. Standard rubber compounds begin to stiffen below 0°C, while cold resistant formulations retain pliability down to -40°C, depending on the specific compound grade. This flexibility ensures proper pulley contact and reduces stress on the belt carcass during operation.
Cold resistant belts incorporate reinforcement layers and cover compounds designed to resist impact damage from falling materials. In cold environments, where the belt cover is more susceptible to impact damage, the compound formulation balances cold flexibility with abrasion resistance to support service life expectations.
Many cold environment applications involve exposure to de-icing chemicals, road salt, or moisture that can affect belt performance. Cold resistant conveyor belt compounds are formulated to resist water absorption and chemical degradation, maintaining belt integrity in conditions where freeze-thaw cycles and chemical exposure are present.
The EP grade selection depends on the minimum operating temperature, required tensile strength, and material load characteristics. For environments down to -20°C, standard cold resistant compounds are sufficient. For temperatures between -20°C and -40°C, enhanced cold resistant formulations with EPDM or specialized compounds should be specified.
Cold resistant conveyor belts are available in widths ranging from 300 mm to 2400 mm, with custom widths available for specific conveyor system requirements. Cover thickness is selected based on the conveyed material's abrasiveness and lump size. Both top and bottom cover thicknesses can be specified independently.
Belt splicing method (mechanical fasteners or vulcanized splices) affects belt end preparation and should be specified during procurement. Cold environment applications may have specific splice requirements to ensure joint performance at low temperatures. Vulcanized splices generally provide longer service life but require on-site equipment and skilled labor.
Standard cold resistant conveyor belts maintain flexibility from -40°C to 50°C continuously. The specific temperature rating depends on the rubber compound formulation and EP grade selected for the application.
Available EP grades include EP100, EP125, EP200, EP250, EP300, EP350, EP400, EP500, and EP600. Each grade corresponds to a specific tensile strength rating measured in newtons per millimeter of belt width.
The minimum order quantity for cold resistant conveyor belts is 100 meters per specification. Orders below this quantity may be accommodated depending on current production scheduling and material availability.
Yes, belt width, length, number of plies, and cover thickness can all be customized to match specific conveyor system requirements. Custom specifications require confirmation during the quotation process.
Production lead time for bulk cold resistant conveyor belt orders is approximately 25 to 35 days. The exact timeline depends on order volume, specification complexity, and current production capacity.